-
We detected your language preference as English. Would you like to switch to the English version for a better experience?
Switch to English
Stay here


Few engineering thermoplastics punish careless datasheet reading as severely as nylon. A single polyamide grade can carry two completely different sets of mechanical values — "dry as molded" and "conditioned" — and the gap between them is not a rounding error. Tensile strength can fall by 20–40%, stiffness by half, while notched impact toughness can double or triple after the material equilibrates with ambient humidity. Engineers who quote dry numbers for a part that will live at 50% RH, or who compare one supplier's conditioned data against another's dry data, routinely discover their design margins were illusory. Understanding where these two data sets come from, what moisture actually does inside the polymer, and how to condition specimens reproducibly is therefore a core competency for anyone specifying polyamide 6, PA66, or their many relatives in structural, electrical, and packaging applications.
| Function | Target Applications | Key Specifications | Compliance Status |
|---|---|---|---|
| PA6 — semi-crystalline engineering polyamide; moisture-sensitive structural resin whose conditioned state delivers very high toughness | Gears, bearings, fasteners, cable ties, fuel-system components, packaging films, automotive trim and underhood clips | Tensile strength ~75–80 MPa dry, ~50–60 MPa conditioned; modulus ~2800–3000 MPa dry vs ~1000–1200 MPa conditioned; water uptake ~2.8–3.0% at 50% RH | UL 94 V-2 (typical, unfilled); UL 746 RTI ratings; FDA 21 CFR 177.1500; EU Regulation 10/2011 (food grades) |
| PA66 — higher-strength, higher-HDT polyamide with slightly lower equilibrium moisture uptake than PA6 | Electrical connectors, sensors, air-intake manifolds, radiator end tanks, industrial and consumer hardware | Tensile strength ~80–85 MPa dry, ~55–65 MPa conditioned; notched Izod ~50–60 J/m dry vs ~100–150 J/m conditioned; water uptake ~2.3–2.5% at 50% RH | UL 94 V-2 to V-0 (FR grades) with UL yellow card; FDA 21 CFR 177.1500; EU 10/2011; RoHS/REACH compliant formulations |
Nylons are built from repeating amide (–CO–NH–) linkages, one of the most polar groups available in a commercial polymer backbone. In the dry state, adjacent chains lock together through interchain hydrogen bonds between carbonyl and N–H groups, and crystalline regions add further order. Water molecules are also strongly dipolar: they diffuse into the amorphous phase, sit between chains, and compete for those hydrogen-bonding sites. Each absorbed water molecule effectively "unzips" a small cluster of interchain bonds, increasing chain mobility in the amorphous domains.
The macroscopic consequence is classical plasticization. Glass transition temperature drops — a dry PA6 may show a Tg around 50–65 °C, but in the fully conditioned state it can fall below room temperature — so stiffness and yield strength decline while ductility, elongation at break, and notched impact energy rise. Because water occupies volume between the chains, the part also swells, mainly in the thickness direction, which changes dimensions and internal stress states. Crystalline regions and the chemistry of the chain itself are not attacked: conditioning is a reversible physical process, not degradation. More background on polyamide chemistry and hydrogen-bond-driven moisture effects in polymers is available in Guidechem's encyclopedia.
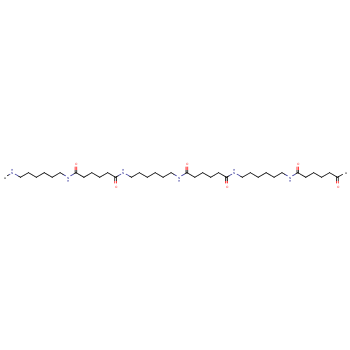
PA66 is produced by polycondensation of hexamethylenediamine and adipic acid, usually via the 6,6 salt:
PA6 is made by ring-opening polymerization of caprolactam, often initiated and balanced with small amounts of water and amines:
Both routes deliver one amide group per six carbon atoms — the structural origin of their similar, and similarly moisture-sensitive, behavior. Increasing the methylene-to-amide ratio (PA11, PA12, PA612) spreads the hydrogen-bonding sites further apart, which is exactly why those specialty nylons absorb far less water.
"Dry as molded" (DAM) data are measured on specimens that have been molded from thoroughly dried resin and tested before appreciable moisture pickup — the strongest, stiffest, most brittle state the part will ever be in. "Conditioned" data are measured after specimens have equilibrated at a defined humidity, most commonly 23 °C / 50% RH as called for in ASTM D618 and the ISO 291 standard atmosphere, giving properties representative of a part in typical indoor service. A third state, saturation (immersion per ISO 62 / ASTM D570), represents the worst-case wet condition. Accelerated conditioning to the 50% RH equilibrium state is possible in humid chambers at elevated temperature (ISO 1110, 70 °C / 62% RH), compressing weeks of diffusion into days.
Moisture absorption by nylons, by weight — the equilibrium values behind every "conditioned" datasheet column. Source: UL Prospector.
With one amide per six carbons and a moderate crystallinity (~30–40%), PA6 absorbs roughly 1.3% water in 24-hour immersion and close to 3% at 50% RH equilibrium, rising toward 9–10% at saturation. The dry material is a stiff, ~2800 MPa engineering resin; the conditioned material behaves almost like a different polymer — visibly tougher, more ductile, and dimensionally larger. PA6 is favored where conditioned toughness matters more than dry stiffness: gears, clips, monofilament, film, and general industrial parts. Typical trade names include Ultramid B, Akulon, and Grilon families.
The slightly more regular chain of PA66 crystallizes more efficiently, giving higher dry strength, higher modulus, and a higher deflection temperature under load than PA6 at the same loading. Its equilibrium uptake (~2.3–2.5% at 50% RH) is marginally lower, but the conditioned-state softening is just as real and must be designed for. PA66 dominates electrical connectors, automotive underhood components, and any application where short-term high-temperature or dry-state rigidity is critical. It is also more notch- and moisture-sensitive in processing: wet PA66 hydrolyzes rapidly at melt temperature.
Stretching the aliphatic segments (PA11 and PA12 have 11 and 12 carbons per amide) cuts the concentration of hydrogen-bonding sites dramatically: PA12 absorbs well under 2% even at saturation, so its dry and conditioned data sets are far closer together. These resins — and PA612, along with PA11 — buy dimensional stability and stable dielectric properties at the cost of dry strength and heat resistance, which is why they are specified for fuel lines, pneumatic tubing, catheters, and precision low-hygroscopic parts. Their limitation is price: they are significantly more expensive than PA6/PA66.
Adding 30–50% glass fiber roughly doubles dry stiffness and strength, but it does not immunize the resin against conditioning effects: the matrix still plasticizes, so conditioned modulus drops 20–40% and notched impact changes substantially, while the differential swelling between glass and matrix introduces warp. Impact-modified and plasticized grades start out tougher and absorb less abruptly; mineral-filled grades trade some toughness for flatter shrinkage. In every class, moisture uptake scales with the resin (matrix) fraction, and the dry-versus-conditioned question never disappears — it merely shrinks.
| Polyamide | CAS Number | Water @ 50% RH, wt% | Saturation Uptake, wt% | Tensile Dry / Conditioned, MPa | Typical Applications |
|---|---|---|---|---|---|
| PA6 | 25038-54-4 | ~2.8–3.0 | ~9–10 | ~75–80 / ~50–60 | Gears, film, cable ties, fasteners, industrial parts |
| PA66 | 32131-17-2 | ~2.3–2.5 | ~8–8.5 | ~80–85 / ~55–65 | Connectors, sensors, underhood, hardware |
| PA6/66 copolymer | — (polymer blend/copolymer) | ~2.5–2.8 | ~8.5–9.5 | ~70–78 / ~48–58 | Flexible clips, tubes, low-warpage parts |
| PA612 | 24936-71-0 | ~1.3–1.5 | ~3.5–4 | ~60–65 / ~50–55 | Precision parts, brushes, fuel-line components |
| PA11 (bio-derived) | 25035-04-5 | ~0.8–1.0 | ~1.8–1.9 | ~50–55 / ~45–50 | Fuel hoses, pneumatic tubing, sports goods |
| PA12 | 24937-79-9 | ~0.7–0.9 | ~1.4–1.6 | ~45–50 / ~42–48 | Medical tubing, cable jacketing, 3D printing |
The table below summarizes the representative dry-versus-conditioned shift that engineers should expect when reading unfilled PA6 and PA66 datasheets, mirroring the source comparison tables:
| Property (unfilled resin) | PA6 Dry | PA6 Conditioned | PA66 Dry | PA66 Conditioned |
|---|---|---|---|---|
| Tensile strength, MPa | 75–80 | 50–60 | 80–85 | 55–65 |
| Tensile modulus, MPa | 2800–3000 | 1000–1200 | 2800–3200 | 1200–1600 |
| Elongation at break, % | 3–10 | >50 | 3–5 | 20–40 |
| Notched Izod impact, J/m | 40–60 | 120–180 | 50–60 | 100–150 |
| HDT @ 1.8 MPa, °C | 65–75 | ~55–65 | 75–90 | ~60–70 |
PA6 and PA6/66 copolymers should be dried in a desiccant dryer at ~80 °C for 2–4 hours; PA66 at 80 °C for 2–4 hours as well, with dew point around −20 to −40 °C. Target residual moisture at the feed throat is ≤0.10–0.20%. Nylon regrind and material left in an open hopper overnight can re-absorb several tenths of a percent from ambient air in humid climates, so hopper drying immediately before processing is standard practice.
Typical melt temperatures are 230–260 °C for PA6 and 260–290 °C for PA66, with mold temperatures of 70–100 °C to promote crystallinity and dimensional stability. Residence time should be minimized at the upper end of the range: molten nylon in contact with moisture undergoes hydrolysis, severing chains and cutting molecular weight — and mechanical performance — permanently.
For property verification, condition specimens at 23 °C / 50% RH per ASTM D618 (typically 40 hours minimum, longer for thick sections) or accelerate to equilibrium in a humid chamber per ISO 1110 (70 °C / 62% RH). For dimensional checks or saturated-state behavior, immerse per ISO 62 / ASTM D570 at 23 °C and report uptake by weight. Production parts are sometimes moisture-conditioned deliberately (hot water or steam) to pre-plasticize them for toughness and dimensional stability before assembly.
| Jurisdiction / Body | Framework | Relevance to Dry/Conditioned Performance |
|---|---|---|
| United States — FDA | 21 CFR 177.1500 (nylon resins, food contact) | Clears nylon resins for food-contact use with extractive limits; conditioned-state migration testing reflects real-use humidity |
| United States — UL (Underwriters Laboratories) | UL 94 flammability; UL 746A/746B (RTI, yellow card) | Long-term thermal index programs test specimens as molded; electrical and flammability ratings underpin connector/insulation specs |
| European Union | Regulation (EU) No 10/2011 (food-contact plastics); REACH; RoHS | Food grades must comply with overall and specific migration limits; moisture state affects diffusion and migration behavior |
| Germany | BfR recommendations (e.g., BfR "Polyamide" kitchenware guidance) | Addresses primary aromatic amines from PA kitchenware, tested under defined aqueous conditioning |
| Japan | Food Sanitation Act; JHOSPA positive list for food-contact utensils | Nylon kitchenware and packaging subject to migration testing with water/food simulants after conditioning |
| International test standards | ISO 291/62/1110/527/75/179; ASTM D618/D570/D638/D648/D256 | Define the conditioning atmospheres and test methods that generate the "dry" and "conditioned" data columns themselves |
"Dry as molded" (DAM) values are measured on specimens tested within a short time of molding from dried resin, typically below 0.2% moisture. "Conditioned" values are measured after the specimen equilibrates at 23 °C / 50% relative humidity (ASTM D618 / ISO 291) — roughly 2.5–3% water for PA6 and ~2.3–2.5% for PA66. The two states bracket the material's real-world behavior between the as-molded extreme and typical indoor service.
Water molecules diffuse into the amorphous phase and hydrogen-bond to the amide groups, replacing chain-to-chain hydrogen bonds. This raises chain mobility — effectively plasticizing the polymer — so yield strength and stiffness fall, while elongation and notched impact energy rise because the material can now deform and blunt cracks instead of fracturing brittlely. The effect is fully reversible by drying and does not alter the chemistry of the chains.
Ambient conditioning at 23 °C / 50% RH follows ASTM D618 or ISO 291 and can take weeks for thick sections because diffusion follows Fick's law with time scaling roughly with thickness squared. ISO 1110 accelerated conditioning (70 °C / 62% RH in a humidity chamber) reaches the equivalent moisture content in a fraction of the time, typically days. Saturated immersion conditioning per ISO 62 or ASTM D570 uses 23 °C water and is reported as weight-percent uptake.
Use conditioned values for anything that will see normal atmospheric humidity — snap fits, clips, structural brackets, long-term stiffness and dimensional layouts — because parts in service drift toward the 50% RH equilibrium within days to months. Reserve dry-as-molded values for hermetically sealed or immediately loaded applications, and always check that comparative datasheets quote the same state. For wet service, also consider saturated properties and the accompanying dimensional swell.
 |
 |
|
 EN
 Agricultural News
 Food News
 Industrial News
 Cosmetic News
 Pharmaceutical News
 Science News

 1YR


