-
We detected your language preference as English. Would you like to switch to the English version for a better experience?
Switch to English
Stay here


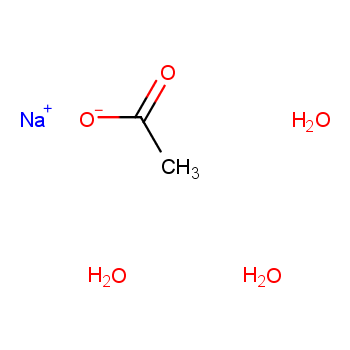
Sodium acetate trihydrate (CAS 6131-90-4) is the crystalline trihydrate of the sodium salt of acetic acid, formula CH3COONa·3H2O, relative molecular mass 136.08. It is a commodity chemical with an unusually wide spread of uses: food additive E262, buffer salt in pharmaceutical and dialysis formulations, phase-change medium in heat packs, and process chemical in textile and water treatment. The anhydrous salt is registered separately under CAS 127-09-3. This paper reviews hydrate stability, the manufacturing route and the compliance perimeter for 2026.
Three properties govern how the material must be bought, shipped and stored. It melts at about 58 °C in its own water of crystallisation, so any drying or warehousing step above that temperature produces a fused, partly dehydrated mass. It effloresces in dry air, converting the surface to the anhydrous form, which depresses assay and generates dust. And it is highly soluble and mildly alkaline in solution, which is why moisture control dominates packaging design.
Commercially this is a high-tonnage, low-margin salt in which logistics and grade documentation matter more than synthesis. Most volume comes from neutralising acetic acid with sodium hydroxide or sodium carbonate and crystallising the trihydrate below its melting point, with bio-based acid increasingly offered as a lower-carbon option. Food, pharmaceutical and technical grades are separated by specification rather than chemistry, so buyers who fail to state grade and packaging receive material that meets neither. CDMO partners encounter the salt as a buffer component and process raw material.
Sodium acetate is the salt of a weak acid and a strong base, so its solutions are mildly alkaline and acetate pairs with acetic acid to buffer around pH 4.76. The trihydrate is a genuine stoichiometric hydrate: three lattice water molecules per formula unit are released, rather than merely desorbed, when the crystal is heated or held in dry air. That explains the sharp melting near 58 °C and the efflorescence that cakes a free-flowing solid, and it is why lattice water must be specified as a stoichiometric component.
Industrial production is an acid-base neutralisation followed by crystallisation that preserves the hydrate. Acetic acid from methanol carbonylation, acetaldehyde oxidation or fermentation is reacted with sodium hydroxide or sodium carbonate, and the solution is concentrated under reduced pressure and cooled. Crystals are separated by centrifugation, washed and dried well below the melting point, then screened to a controlled particle size. Drying most often destroys the product and deserves the tightest control.
Three shifts shape 2026. Demand for lower-carbon acetate is growing as brand owners push bio-based content, pulling producers toward fermentation-derived acid. Dialysis and parenteral volume continues to grow, raising the share of compendial grades. Heat-pack and industrial demand is more cyclical, tied to winter seasons and to textile activity, so documented grades gain share while commodity volume stays flat.
Capacity follows acetic acid, so it sits where the acid is cheapest: Asia-Pacific, and China in particular, dominates acetic acid output and therefore acetate salt volume, with substantial capacity in North America and Europe tied to local acetyl chains. Export flows run east to west, although freight economics limit how far a low-value hydrate travels profitably. Compendial grades are less trade-exposed because qualification cost keeps them near the customer, and supply risk is feedstock driven.
Pricing tracks acetic acid and caustic soda or soda ash almost directly, with a smaller contribution from evaporation and drying energy. Food and compendial grades carry a premium over technical material that reflects testing, documentation and segregation rather than the salt itself, and low-endotoxin grades command a further step. Freight matters unusually relative to value, because the product is dense, bulky and low priced per kilogram, so delivered cost often decides the supplier.
A simple salt still sits inside several regimes at once: as a food additive it needs authorisation and purity criteria, as a pharmaceutical buffer it needs a monograph and documented excipient cGMP, and as a chemical it needs inventory registration and a safety data sheet. ICH Q7 and ICH Q11 apply where an acetate salt is a drug-substance component, but here the controlling documents are the USP and Ph.Eur. monographs, an excipient DMF where required, and ISO 9001. No CEP is needed, since compendial conformity is demonstrated directly.
The environmental profile of this salt is dominated by its acid precursor and by evaporation energy. Acetic acid from methanol carbonylation carries petrochemical emissions, whereas fermentation-derived or recovered acid offers a lower footprint, and concentrating the salt is steam intensive. Buyers with published targets now ask for cradle-to-gate data and ISO 9001 and ISO 14001 certification, particularly where the acetate enters food or healthcare products.
Emissions concentrate in acetic acid manufacture, in steam for evaporation and crystallisation and in drying, with transport adding a meaningful share because the product is bulky and low valued. Abatement runs through bio-based or recovered acid, mechanical vapour recompression and multi-effect evaporation, heat recovery, renewable electricity and regional production to cut freight. Reporting now expects primary Scope 1, Scope 2 and Scope 3 data from acid suppliers rather than generic factors.
Traceability expectations cover the acetic acid route, the alkali source, the crystallisation water and the absence of animal-derived processing aids. Buyers should require lot-level linkage to acid and alkali batches, a bio-based content declaration supported by mass-balance evidence, and conformity to additive purity criteria for food grade. Controls combine ISO 9001 and ISO 14001 certification, ESG disclosure, audits and change control on crystallisation and drying.
This is a dense, low-value, moisture-sensitive crystalline solid shipped in 25 kg bags or in bulk, so freight economics and packaging integrity jointly determine delivered quality. The material effloresces in dry air and fuses if heated through its melting point, which can happen inside a container in a hot climate. Logistics requirements belong in the supply agreement, including maximum storage temperature, packaging barrier and the action after heat exposure.
Sodium acetate trihydrate is not a dangerous good under UN Model Regulations, ADR, IMDG or IATA rules and moves as general cargo with a GHS-format SDS. The risks are thermal: a container reaching the melting point arrives as a fused block that cannot be discharged without breaking the packaging, so ventilated stowage should be specified in hot seasons. Because a food-ingredient declaration faces different import controls from an industrial salt, invoice, packing list and SDS descriptors should be aligned before dispatch.
Competitive advantage in a commodity salt comes from grade discipline and delivered reliability rather than from chemistry. A producer that holds hydrate stoichiometry through drying and transit, and that supplies food, compendial and technical grades from one plant under separated documentation, wins contracts that price-focused competitors cannot hold. Three measures drive that outcome.
Sodium acetate trihydrate looks like the simplest possible product and is in practice a test of specification discipline. The chemistry is one neutralisation, but the hydrate is fragile: it loses water in dry air, melts at a temperature a hot container reaches, and cakes if stored too long. Value sits in delivering a specified hydrate in a specified grade, in packaging that survives the journey.
For buyers, the 2026 agenda is to specify the hydrate and assay basis explicitly, set a maximum storage temperature in the supply agreement and qualify on documentation rather than price. Technical material must never be represented as food additive E262 or as compendial grade, and no dosing guidance or health claim belongs in B2B documentation. Where CDMO support is engaged for buffer development, method validation or custom packaging, the work is a B2B service to pharmaceutical, food and industrial partners.
Powered by Guidechem
This white paper is exclusively compiled by the Guidechem Intelligence Team based on global customs data, regulatory databases, and industry research. Guidechem is a leading global B2B chemical platform, dedicated to connecting global buyers with verified, high-quality manufacturers.
Relying on Guidechem's extensive global database, we have mapped the core participants in the current global Sodium acetate trihydrate supply chain:
Disclaimer: The content of this white paper is compiled based on public market data and regulatory information available as of 2026. Global chemical regulations are subject to dynamic adjustments. In actual export operations, enterprises must consult professional regulatory advisors or relevant competent authorities to obtain the latest compliance guidance.
|
 |
 |
 |
 |
 |
 EN
 Agricultural News
 Food News
 Industrial News
 Cosmetic News
 Pharmaceutical News
 Science News

 2YRS

